
Composite tooling
Four Routes to a Composite-Tooling Master Model
Four ways to build a composite-tooling master: compare lightweight layered construction, cast-resin blanks, steel-framed structures and bonded tooling board against the actual mould-making process.
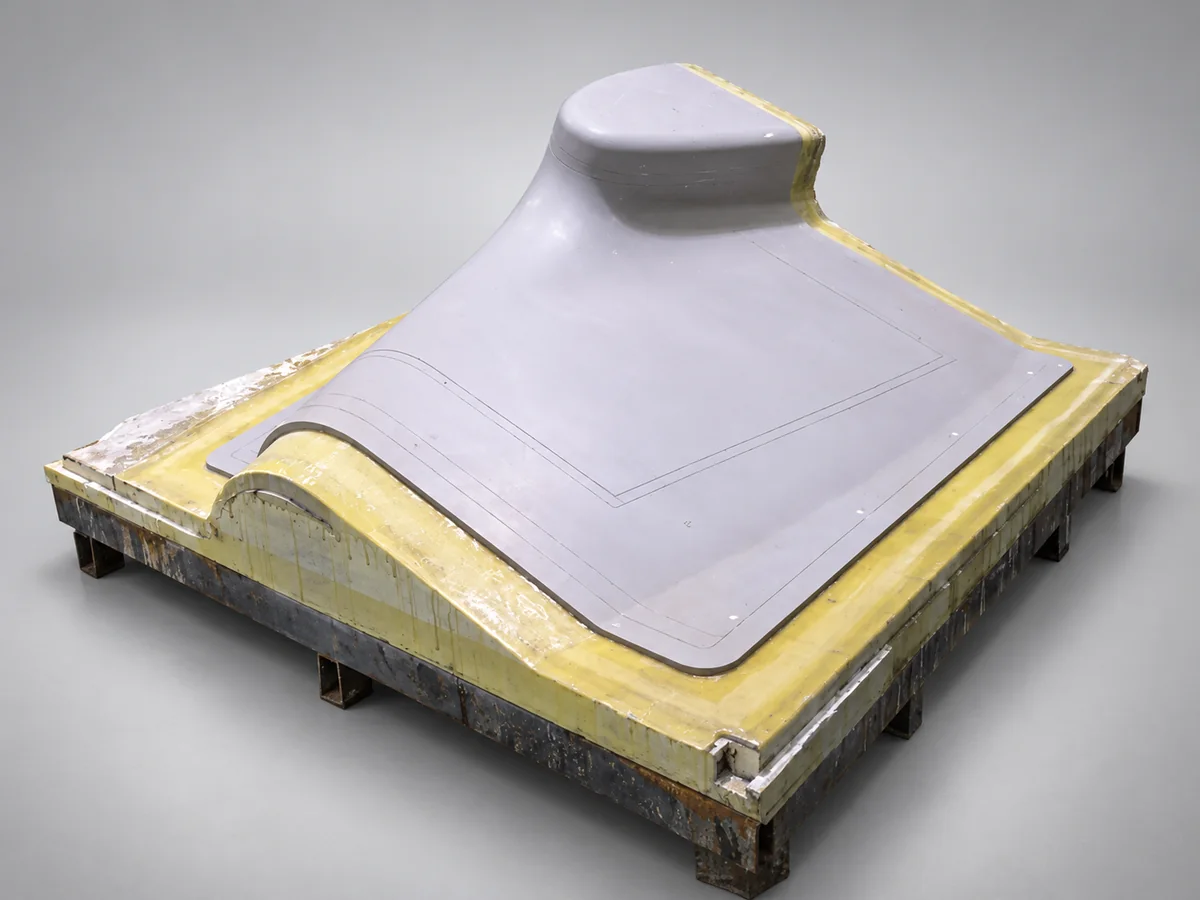
A master model is the reference surface from which a production mould is made. Its geometry and surface finish are transferred to the mould; its dimensional stability determines how faithfully that transfer takes place. A master is often a positive form, or plug, but the term describes its function rather than a particular shape.
The distinction between master and production mould matters when choosing materials. The production mould must withstand the conditions used to manufacture parts. The master must withstand the conditions used to make that mould. Those thermal cycles can differ substantially, particularly when the mould is released from the master before post-curing.
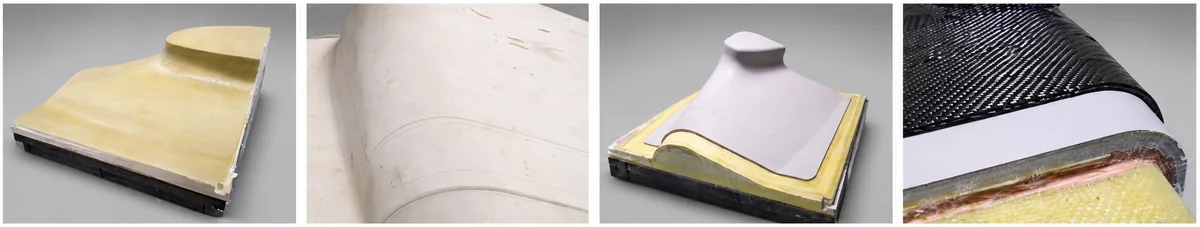
Four practical construction routes
1. Polyurethane foam, glass fibre, tooling paste and gel coat
This route separates bulk from precision. A lightweight polyurethane foam core provides the overall volume, a glass-fibre/epoxy skin provides a supporting shell, and a machinable tooling-paste layer defines the final surface.
The foam is machined with allowance for the subsequent layers. The glass-fibre skin is applied and, where the process permits, vacuum-compacted to reduce voids. A compatible primer and tooling paste are then applied to the required thickness. After the specified cure and post-cure, the paste is CNC-machined and finished with a compatible tooling gel coat. Curing, sanding and polishing complete the surface preparation.
This construction is useful for complex shapes that would require extensive machining from a solid blank. Its success depends on the compatibility of the foam, laminate, paste, primer and surface coating. Application windows, layer thicknesses and cure schedules must come from the selected material system; they are not interchangeable between grades. A lightweight core is an advantage in handling, but it does not establish the temperature capability or dimensional stability of the complete master.
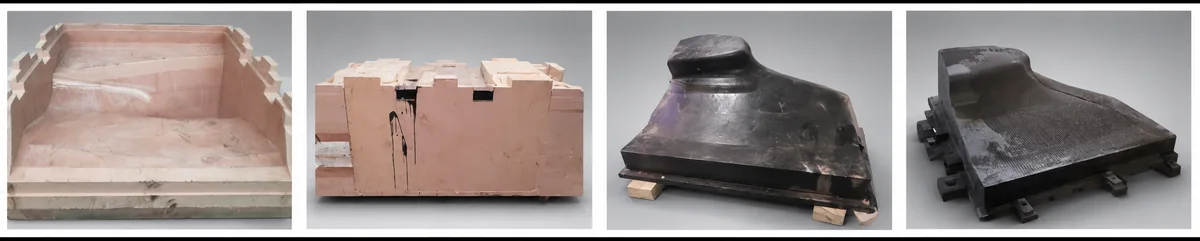
2. An integral cast-resin blank
Here, the machinable blank is cast rather than assembled from board. A disposable or demountable mould box is prepared, treated for release and filled with a suitable polyurethane or epoxy casting system. The blank is cured and post-cured as specified, then rough- and finish-machined to establish the surface, datums and mounting features.
The main advantage is a continuous machining surface without board joints. The main challenge is controlling the casting process. Section thickness, resin volume, exotherm and shrinkage must be assessed together. The casting depth and any staged-pour procedure must follow the chosen system's requirements. Fillers, inserts or reinforced skins may be useful in a validated design, but are not universal substitutes for controlling heat and cure.
Inspection should address voids, residual stress and distortion as well as the machined dimensions. For a master where surface continuity is particularly valuable, the extra work of making a mould box and controlling the casting can be justified.
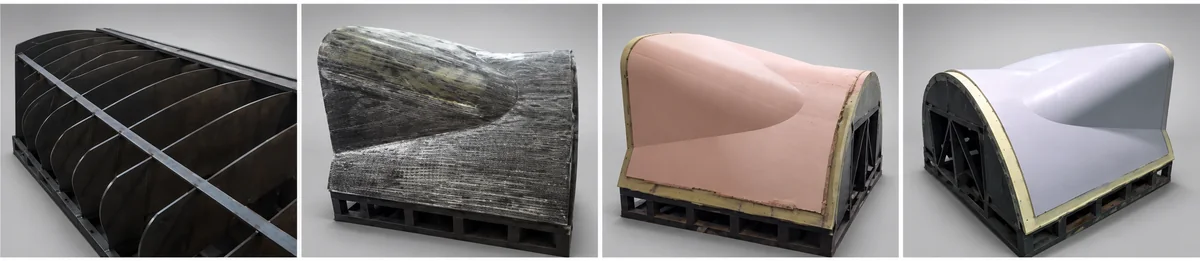
3. A contoured steel frame with a glass-fibre skin and tooling paste
Large or slender masters often benefit from a frame that carries the structural loads while the outer layers establish the working surface. A steel frame follows the approximate contour. A glass-fibre/epoxy skin spans the structure, and a machinable tooling-paste layer is applied and finished with a compatible gel coat.
Frame fabrication, stress management and datum control are central to this route. Locating surfaces should be established and checked before the surface is developed. The skin and its interfaces require inspection and, where the mould-making process uses vacuum, leak testing.
Thermal expansion also needs attention: steel, laminate, paste and coating respond differently to temperature. Any conditioning cycle before final machining must remain within the limits of every constituent and follow the validated material schedules. This architecture can avoid an unnecessarily massive solid blank, but adds interfaces that must remain stable and sealed throughout mould manufacture.
4. Machining a master from a bonded tooling-board blank
Factory-cured polyurethane or epoxy tooling board offers a direct route to a stable, machinable blank. Boards are cut into layers or blocks, the mating faces are prepared, and the pieces are bonded with a compatible structural adhesive. A fixture or locating pins maintain alignment during cure. Once fully cured, the assembly is CNC-machined from common datums.
Select the board for the thermal cycle the master will actually experience. The production mould's eventual operating temperature is an important design input, but it is not necessarily the temperature reached by the master. If the tooling system permits initial cure on the master and post-cure after release, assess those stages separately and verify that the mould remains properly supported during post-cure. Density alone is not a selection criterion: heat-deflection temperature (HDT), glass-transition temperature (Tg), coefficient of thermal expansion (CTE) and permitted operating temperature describe different properties and must be read with their test conditions.
Accuracy belongs to the bonded assembly, not just the board. Match the adhesive, surface preparation and support to the thermal cycle; allow full cure, then inspect and seal the joints. Temperature differences between machining, inspection and mould copying can affect dimensions. Allow the blank to equilibrate at a defined reference temperature and verify geometry, release performance and vacuum integrity where required.
This route is attractive when inspection, repair or design changes are likely. Its trade-offs are joint control, material utilisation and machining time. Compare the full cost of board, adhesive, machining, sealing and later modifications with the other routes, rather than comparing board prices alone.
Compare the complete construction
The four routes solve different combinations of geometry, stiffness, surface quality and manufacturing effort. None can be selected reliably from a material name or density figure alone.
| Route | How the surface is made | Reasons to consider it | Key controls |
|---|---|---|---|
| Foam, glass fibre and tooling paste | Machined paste on a reinforced lightweight core | Complex shapes; reduced solid-stock removal | Layer compatibility, voids, paste thickness and thermal limits |
| Integral cast-resin blank | Machining a cured, continuous casting | A surface without board joints | Exotherm, shrinkage, cure, voids and mould-box design |
| Steel frame, glass-fibre skin and paste | A machined outer layer on a structural frame | Large or slender geometries | Frame stability, datums, differential expansion and sealed interfaces |
| Bonded tooling board | Machining a bonded, factory-cured blank | Accessible CNC machining; inspection, repair and design changes | Adhesive compatibility, joint quality, reference temperature and material utilisation |
Start with the mould-making process
Before choosing a route, define the master's actual thermal cycle, the number of moulds to be copied, the required surface finish, any vacuum requirements, the handling arrangements and the available CNC envelope. Establish how the master will be supported and inspected, and how the finished mould will be released and post-cured.
A suitable material system is only part of the solution. Reliable geometry also depends on sound datums, complete cure, stable interfaces and a controlled reference temperature. Comparing those requirements across the complete construction gives a more useful basis for selection than a headline material property.